
Titanium and titanium alloy bar billets have low thermal conductivity. During the hot extrusion process, the temperature difference between the surface and the inner layer is large. During the extrusion process, the temperature difference on the surface of the extrusion cylinder can reach 200-250 degrees. Due to the large temperature difference between the suction strengthening and the blank section, the metal material on the surface and the center of the blank will have very different strength and plastic properties, and very uneven deformation will occur during the extrusion process. The larger additional tensile stress becomes the root cause of the surface cracking of the extruded product. The results show that the hot extrusion process of titanium rods and titanium alloy rods is more complicated than that of aluminum alloy, copper alloy, and even steel, which is determined by the special physical and chemical properties of titanium rods and titanium alloy rods.
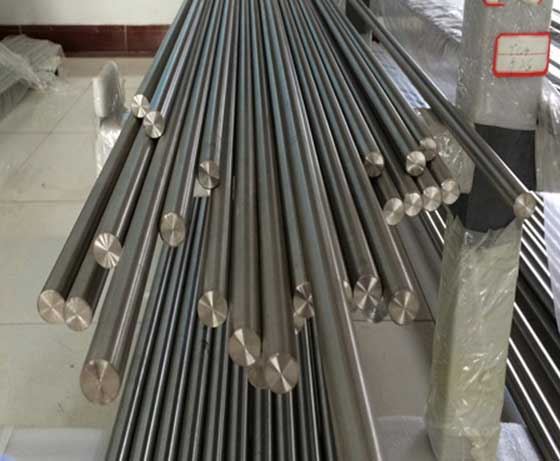
Through the research on the metal flow kinetics of industrial titanium alloys, it is found that the metal flow behavior is very different in the corresponding temperature zone of each alloy. Therefore, the heating temperature of the billet, which determines the phase transition state of the metal, is one of the main factors affecting the extrusion flow characteristics of titanium rods and titanium alloy rods. Compared with the extrusion temperature in the p phase zone, the extrusion flow in the a a+P phase zone is more uniform. It is very difficult to obtain high surface quality for extruded products. Prior to this, the extrusion of titanium alloy bars must use lubricating oil. The main reason is: titanium and iron-based alloy or nickel-based alloy mold materials form a fusible eutectic at 980 and 1030°C, causing intense wear of the mold.
The main factors affecting metal flow in the extrusion process
1. The method of extrusion. The back extrusion has a uniform flow, which is more uniform than the forward extrusion metal, and the cold extrusion has a uniform flow than the unlubricated extrusion metal, and the lubricated extrusion fluid flows evenly. By changing the friction conditions, the effect of the extrusion method is achieved.
2, extrusion speed. Increasing the extrusion rate aggravates the unevenness of metal flow.
3. Extrusion temperature. Increase the extrusion temperature, reduce the deformation resistance of the blank, and aggravate the uneven metal flow. In the extrusion process, when the heating temperature of the extrusion cylinder and the die is too low, and the temperature difference between the outer layer and the center layer is large, the unevenness of the metal flow increases. As the thermal conductivity of the metal increases, the temperature distribution on the end surface of the ingot is gradually uniform.
Fourth, mental strength. Other things being the same, the higher the strength of the metal, the more uniform the flow.
5. Modular angle. Die angle rate (that is, the greater the angle between the end face of the mold and the central axis, the worse the fluidity of the metal. When the porous die is extruded, the die hole arrangement is reasonable, and the metal flow tends to be uniform.
6. Deformation degree. Deformation that is too large or too small will cause uneven metal flow.


