
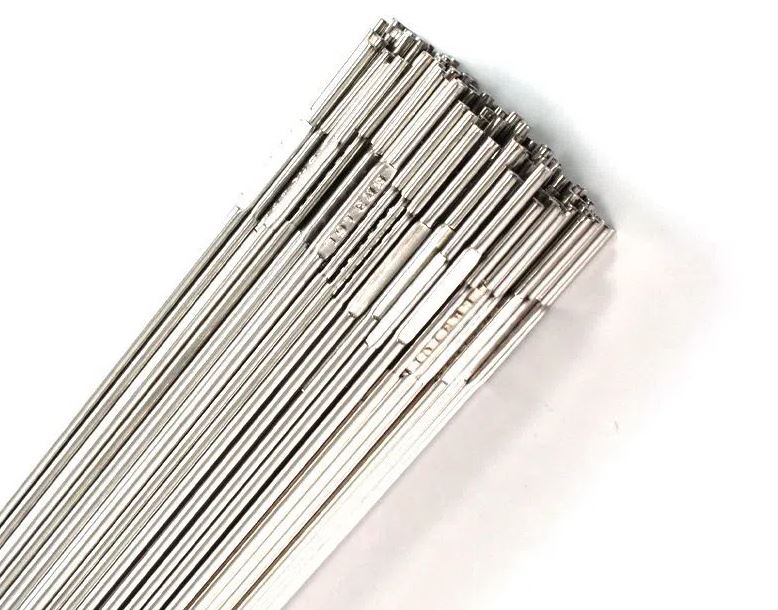
Titanium welding bars are very important to prepare for welding, pre-welding preparations mainly include: pre-welding cleaning: before welding with a fine wire brush of stainless steel bevels and bevels on both sides of the 50mm range of titanium alloy surface grinding, until the titanium alloy itself to reveal the metal luster. After grinding, use a clean white silk cloth with acetone to wipe the bevel and its two sides clean, in order to thoroughly remove the oxide film, grease, water, dust and other debris in the welding area. Commissioning equipment: Before welding, carefully check the pressure of the gas cylinders to ensure that the pressure of various gases is sufficient. When adjusting and checking, the welding gun can generally be walked over the full length of the weld to ensure that the walking mechanism is working properly and that the gun is ideally aligned with the weld.
Plasma arc welding (PAW) of the ion gas, nozzle shielding gas, shield and back shielding gas are used a pure argon (≥ 99.99%); laser welding (LW) process side blowing gas using pure helium (≥ 99.99%), dragging shield and back shielding gas with a pure argon (≥ 99.99%); laser + molten electrode gas welding (LW + MIG) of the composite welding when the MIG torch using ( 70%He+30%Ar) gas mixture. The base materials for the welds are Ti70 (Ti-2.5Al-2Zr-1Fe alpha titanium alloy) and TA5 (Ti-4Al-0.005B alpha titanium alloy). The welding consumables were all made of TA10, a disc-shaped wire with a diameter of 1.2mm.
After welding, the appearance of the weld was inspected and non-destructive testing was carried out. The colour of the titanium alloy can indicate the degree of contamination produced by the weld. General silver-white protection is excellent, there is almost no harmful gas pollution; light yellow, golden yellow weld on the mechanical properties of the impact is not significant; other blue, grey and other colours are not acceptable. Due to the high temperature zone to take the protection of adequate, after welding the appearance of the weld colour is basically silver-white or golden yellow. However, the protection effect is slightly worse at the starting arc because the dragging cover cannot be fully leaned firmly in the starting arc section. Under normal circumstances, the appearance of the weld after inspection is well formed, no cracks, unfused, porous, weld tumour and other defects.


